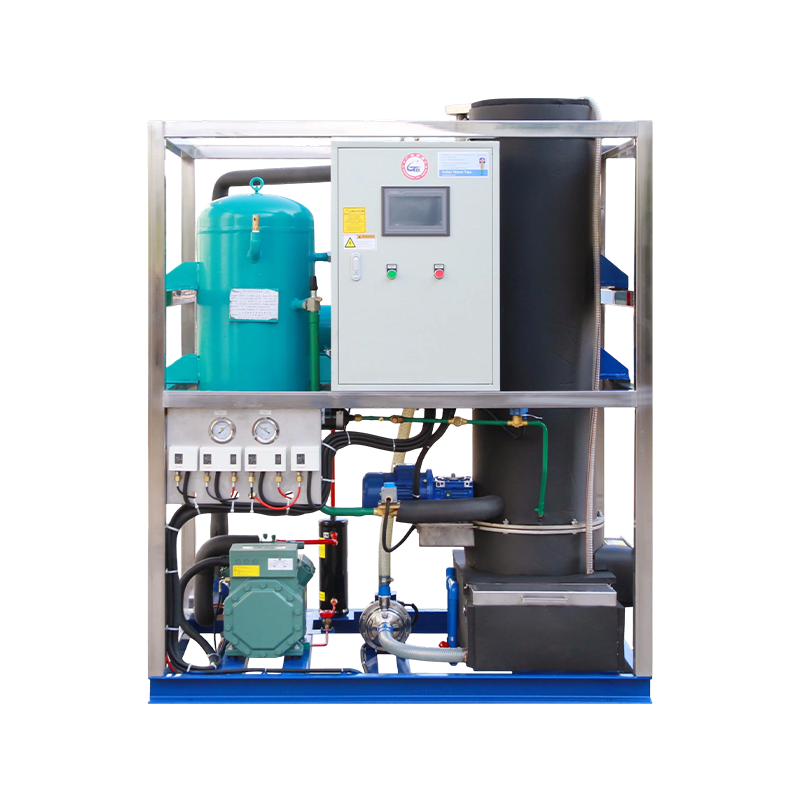
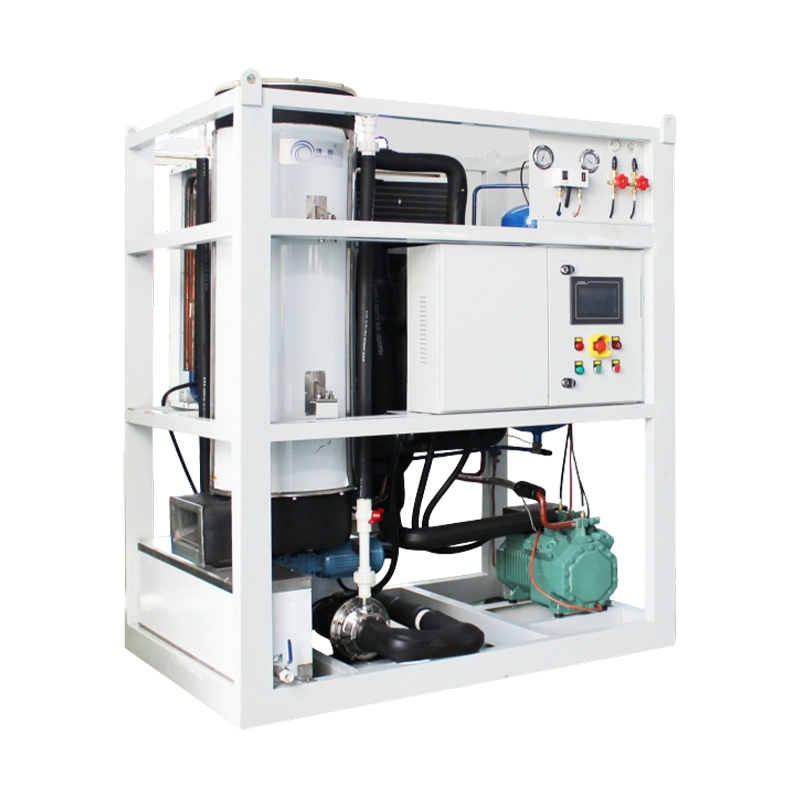
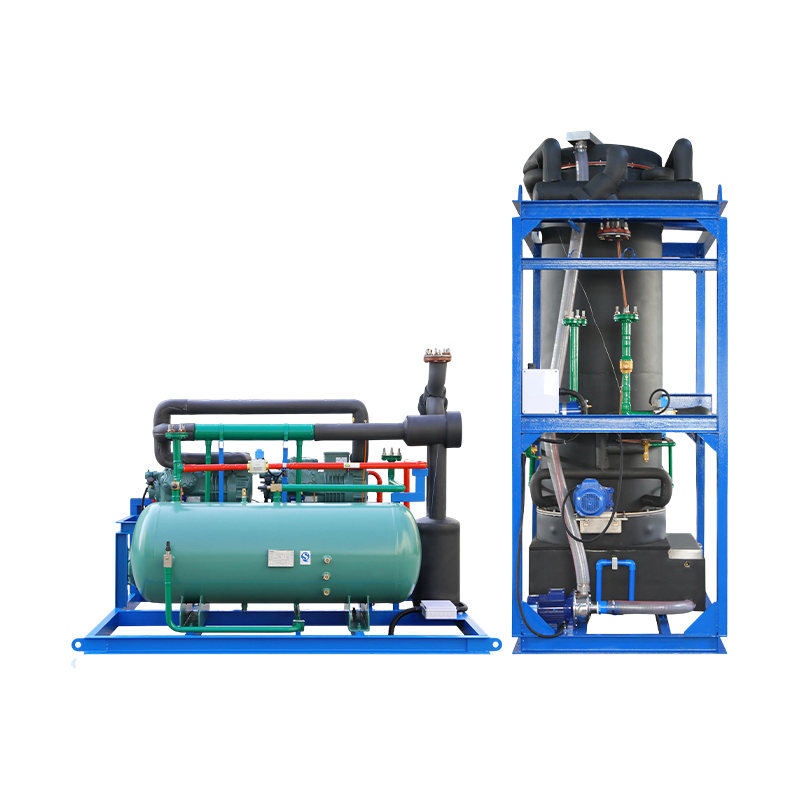
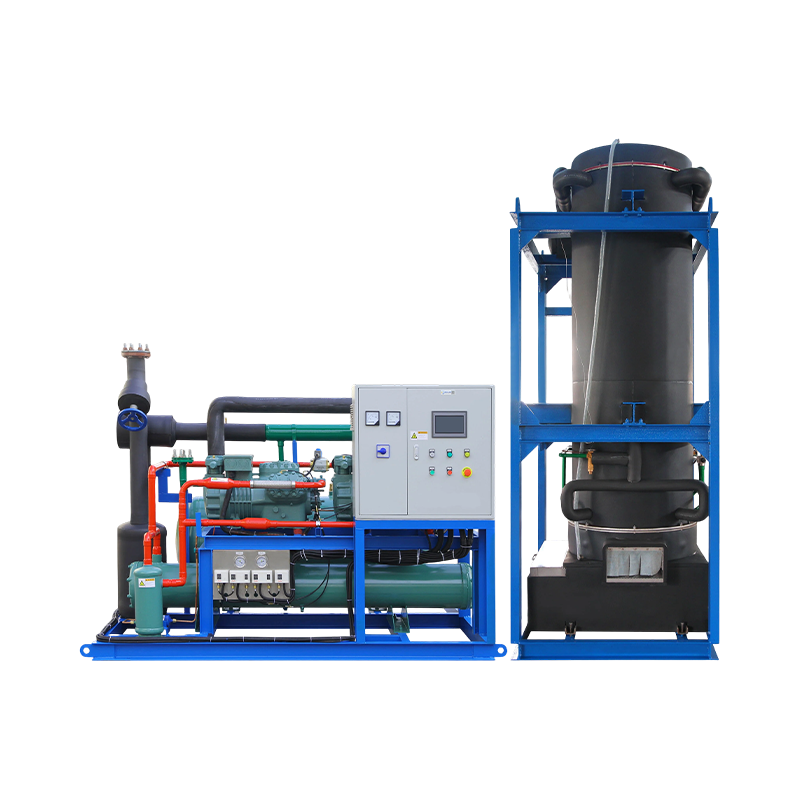
Home / Product / Ice Making Machines / Tube Ice Machine
Ice Making Machines
Continuously provide reliable, efficient and application-
oriented refrigeration equipment to end customers and engineering partners in various markets.
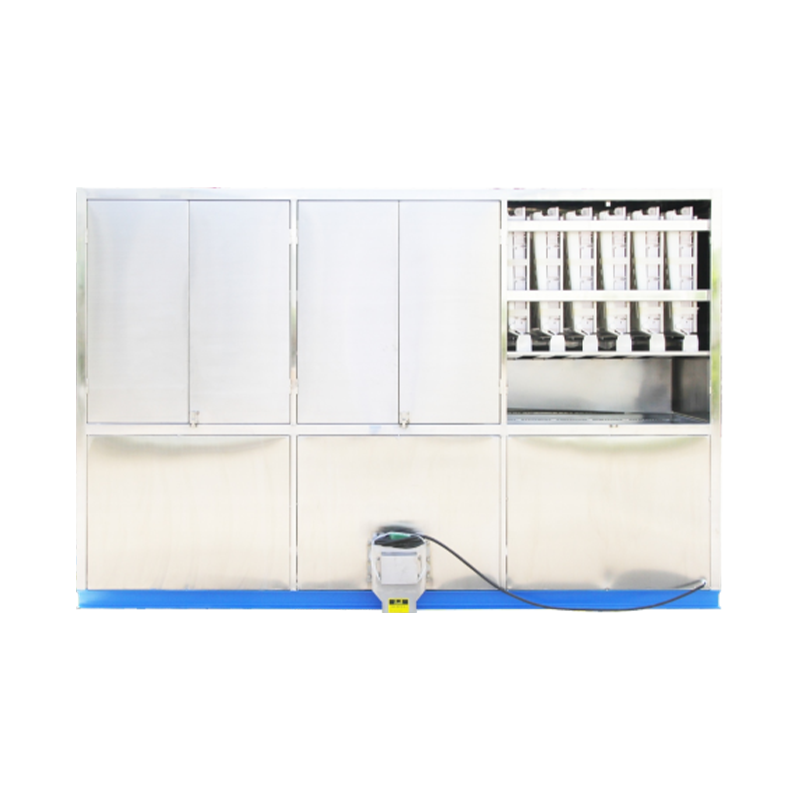
  • Tube Ice Machine
  • Tube Ice Machine
  • Tube Ice Machine
  • Tube Ice Machine
  • Tube Ice Machine
  • Tube Ice Machine
  • Tube Ice Machine
  • Tube Ice Machine
  • Product Details
  • FAQ

Applications
Fresh Seafood Cooling: Provides hygienic ice for aquatic product storage, processing, and transportation.
Food Transportation Preservation: Maintains low temperatures for fresh meat, frozen goods, and cold chain logistics.
Fruit & Vegetable Fresh Keeping: Supports harvesting, sorting, and temporary storage to reduce freshness loss.
Beverage & Catering Use: Supplies clear ice for cocktails, cold drinks, hotels, bars, and milk tea shops.

Core Feature
1. Food-Grade Structure: All ice contact parts use SUS304 stainless steel, meeting HACCP hygiene requirements for safe ice production.
2. High-Quality Ice Output: Produces crystal-clear tube ice with high hardness and slow melting speed, extending cooling performance by approximately 30% compared with ordinary ice.
3. Direct Edible Ice Production: Generates pure ice with low impurity levels and high sanitary standards, suitable for food and beverage applications.

OEM/ODM Services
We support OEM/ODM customization based on customer logos, specifications, technical requirements, and designs. Our team provides assistance from structural design and prototype development to testing and mass production, delivering customized Tube Ice Machine products that meet different market requirements.

Item Details
MOQ 1 unit
Delivery Time 60–90 days
Shipping Method By sea
Payment Terms T/T, L/C at sight

Quality Certification
Tube Ice Machine complies with 3C certification requirements and is manufactured under an ISO 9001 quality management system, ensuring consistent quality control, reliable performance, and standardized production processes.

FAQ
1. What industries commonly use a Tube Ice Maker?
A Tube Ice Maker is widely used in seafood processing plants, food distribution centers, supermarkets, restaurants, and beverage production facilities where continuous ice supply is required.

2. How is an Industrial Tube Ice Machine different from regular ice-making equipment?
An Industrial Tube Ice Machine is designed for higher production capacity and longer operating cycles, making it suitable for large-scale commercial cooling and preservation applications.

3. Can an Automatic Tube Ice Machine reduce manual operation?
Yes, an Automatic Tube Ice Machine integrates automatic ice-making and harvesting functions, helping reduce labor requirements and improve production efficiency.

Parameter Specification
Output Capacity 1–30t/24h
Ice Outer Diameter Φ22, Φ28, Φ32, Φ38
Ice Inner Diameter Φ10, Φ12, Φ14, Φ16
Ice Length 25–60mm
Cooling Type Air Cooling / Water Cooling
Power Supply 380V 50Hz, 3P
Jiangsu Bolang Environmental Technology Co.,Ltd.

Industry Experience

ABOUT US
About Bolang

Founded in 2012, Bolang designs and manufactures ice machines, quick freezing equipment, industrial chillers and refrigeration units.

With integrated capabilities in refrigeration system design, equipment manufacturing, automatic control and factory testing, Bolang serves food processing, cold storage, chemical, pharmaceutical and other industrial applications.

Discover Bolang
  • 10000

    Manufacturing Facility

  • 1000+

    Customers Served

  • 12 Million

    Registered Capital

News
2026-08-18
1110/5000 The market for spiral freezing machines has witnessed a strong growth, with the Asia-Pacific region and food processing forming the core engines.

Dual or Single Drum Operation: Diversified Technical Routes to Meet Diverse Scenarios
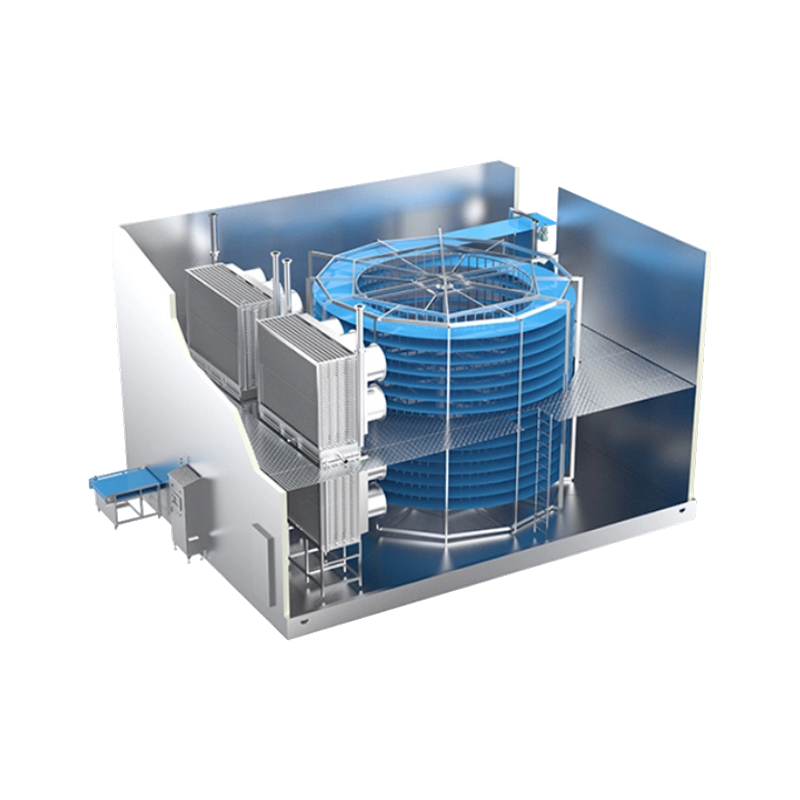
Currently, the spiral freezing machine market has adopted a three-pronged technical route of single drum, double drum, and self-stacked conveyor belt to meet the differentiated demands of various food processing scenarios.

The single drum spiral freezing machine, as the mainstream model, is suitable for medium- to large-scale continuous freezing of aquatic products, meat, and baked goods. With a mature and stable refrigeration system and moderate floor space requirements, it occupies the largest market share. The double drum spiral freezing machine, on the other hand, achieves greater production output under the same floor space conditions, and its optimized net belt running path and cold air circulation efficiency make it particularly suitable for large meat processing plants, poultry processing enterprises, and other high-demand scenarios requiring extremely high unit area production capacity. Meanwhile, new-generation products represented by the self-stacked spiral freezing device of Sifang Technology, through innovative design of the transmission system, enable the self-stacking of the net belt and operation, and in combination with intelligent control and reverse air flow technology, improve heat exchange efficiency while further compressing floor space, becoming an important direction for the industry's future evolution.

Technical Upgrade as the Main Theme: Energy Efficiency, Intelligent Control, and Low-Carbon Refrigeration Moving Forward Together
Facing global energy price fluctuations and the intensification of "carbon neutrality" policies, the spiral freezing machine industry is undergoing a profound transformation from "solely pursuing production capacity" to "optimal energy efficiency throughout the life cycle".

In terms of energy-saving technology, energy recovery devices, efficient variable-frequency compressors, and heat-air defrosting optimization have been widely applied in the new generation of equipment, helping food processing enterprises significantly reduce unit tonnage electricity consumption. In terms of intelligent management, the integration of IoT sensors and predictive maintenance systems has become the core selling point of leading manufacturers - through real-time monitoring of evaporator frosting status, fan operating parameters, and net belt load, the system can automatically adjust refrigeration capacity and operation rhythm, ensuring consistent and stable center temperature of frozen products and stability of quality, while significantly reducing the risk of unplanned downtime. Additionally, the global regulatory trend towards stricter control of low GWP refrigerants (such as CO₂, ammonia, HFOs) is forcing manufacturers to accelerate the elimination of high GWP refrigerant solutions and adopt more environmentally friendly refrigeration system designs, which has become an "entry threshold" for entering the EU and North American high-end markets.

Application Scenarios Continuously Penetrate: Beyond Meat and Seafood
Due to their compact floor space, stable production capacity, and uniform cooling, the application scope of spiral freezing machines has expanded from traditional meat and poultry and aquatic product processing to baking pastries, pre-prepared dishes, dairy products, ice cream, seasonings, and other emerging fields. Especially with the explosive growth of the global frozen food and ready-to-eat food markets, spiral freezing systems with "fast passage" and "flexible production" capabilities are becoming the preferred solution for food processing enterprises for production line upgrades.

Competitive Landscape and Overseas Expansion Wave: Chinese Enterprises Accelerating the Capture of Global Shares
From the global competitive situation, international giants such as GEA, JBT Corporation, Marel, and FPS Food Process Solutions still occupy the first echelon, but their market shares are being challenged by Chinese enterprises represented by Sifang Technology, Ice Wheel Environment, Dalian Ice Mountain, and Fujian Snow, with their complete supply chain support, rapid response to customized services, and more competitive cost performance. Chinese enterprises not only rapidly penetrate emerging markets such as Southeast Asia and South America but also start to export technologies and complete line solutions to European and North American high-end markets.

Read More
2026-07-20
The market for pipe ice machines is expanding rapidly, with the Asia-Pacific region leading global growth.

As the food cold chain, chemical cooling, and supermarket retail industries continue to expand worldwide, the market for pipe ice machines, an important branch of artificial ice production, is experiencing a new round of rapid growth. The latest industry report shows that the global market for pipe ice machines exceeded $447 million in 2025 and is expected to exceed $743 million by 2035, with a compound annual growth rate of over 5.2%. In this growth wave, the Asia-Pacific region, driven by population growth and rapid urbanization, is expected to occupy 40% of the global market share by 2035, becoming the undisputed main engine.

Technological iteration: From "ice making" to "intelligent ice", energy efficiency and intelligence are the core competitiveness.
Currently, the pipe ice machine industry is undergoing a profound transformation from traditional mechanical manufacturing to efficient energy conservation and intelligent management. Against the backdrop of energy conservation and emission reduction becoming a global consensus, the new generation of pipe ice machines, through optimizing the evaporator structure and adopting efficient open-type screw compressors, significantly reduces the unit ice-making power consumption, meeting the strict cooling requirements of industries such as dyes and chemicals for reaction vessels. For example, the energy-saving pipe ice machine exhibited by Xie Ren Group, with its modular design and dual-loop heat gas de-icing technology, not only achieves rapid ice production and continuous ice supply, but also significantly improves energy efficiency through optimized refrigeration cycles.

At the same time, the integration of Internet of Things and artificial intelligence technologies is reshaping the equipment operation mode. Modern pipe ice machines are gradually integrating remote monitoring and intelligent management systems, enabling fault warning and automatic adjustment, not only improving operational efficiency but also effectively reducing labor costs and downtime risks. For example, Guangzhou Koller Refrigeration recently obtained the "bucket pump liquid supply system" patent, through precise control of refrigerant supply and heat gas de-icing optimization, further enhancing the stability and energy efficiency of the system.

Application scenarios are expanding deeply: not limited to aquatic products and edible ice
Due to its unique hollow tube structure, pipe ice machines have a large heat exchange area, are not prone to melting, and have good fluidity. Their application fields have far exceeded the traditional scope of aquatic product preservation.

In the food processing industry, pipe ice is widely used in meat processing, supermarket fresh product display, and restaurant beverage refrigeration; in the industrial field, pipe ice machines have become an indispensable "cold source cornerstone" in industries such as dye synthesis, concrete cooling, and chemical reaction vessel cooling. Research data shows that the food processing sub-market is expected to occupy 35% of the pipe ice machine application market by 2035, while stable demand in the fishing and chemical industries provides a solid foundation for the market.

Regional pattern and enterprise trends: Made in China leads the world
From the regional competition pattern, China is not only the largest single market for pipe ice machines globally, with its share exceeding the combined total of North America and Europe, but also an important equipment exporter.

Read More
2026-07-08
The new generation of screw parallel compression condensing units help upgrade the large and medium-sized cold chain industry.

Recently, in response to the increasing demands for refrigeration in scenarios such as pre-prepared food industrial parks, aquatic product processing bases, large-scale cold storage logistics parks, and pharmaceutical constant-temperature storage, the new generation of screw parallel compression condensing units have been officially launched. The units rely on a multi-head modular parallel architecture, PLC intelligent group control, and efficient condensation integration design. With core advantages such as load adaptive regulation, redundant safe operation, high comprehensive energy efficiency, and convenient operation and maintenance, they provide a stable refrigeration solution for large and medium-sized low-temperature cold storage and rapid freezing production lines, helping to reduce electricity costs, stabilize storage, and ensure product safety in cold chain projects.

In traditional large and medium-sized refrigeration projects, multiple independent single-unit units often have problems such as poor load matching, high idle energy consumption, no redundant backup, and complex machine room pipelines. Once a single unit fails, it can easily cause temperature fluctuations in the warehouse and the entire rapid freezing production line to stop, resulting in loss of high-value products such as aquatic products, pre-prepared foods, and pharmaceuticals. This screw parallel compression condensing unit adopts a multi-unit screw compressor parallel networking solution, equipped with an intelligent group control system, which can automatically schedule the start and stop of compressors and energy loading according to the real-time cold load of the warehouse area, achieving demand-based output of cooling capacity, avoiding energy waste caused by "big horses pulling small carts", and significantly reducing the overall energy consumption compared to traditional decentralized single-unit schemes.

The core of the unit uses high-efficiency screw main units, optimizes rotor profile design, and is equipped with an efficient oil separation device, with high oil separation efficiency, ensuring long-term lubrication of the machine heads; the entire system integrates oil separators, manifold pipes, liquid storage, condensation heat exchange, and safety protection modules, with an organized and compact layout, significantly reducing the floor space of the machine room. The complete multi-level safety protection system covers multiple warnings such as high and low pressure, oil pressure, overload, phase sequence, exhaust temperature, and liquid strike protection, real-time monitoring the operation status of the unit; the unique redundant design allows other units to continue to undertake the refrigeration load when a single compressor is under maintenance or fails, without the need for overall shutdown, maintaining the control of the warehouse temperature, meeting the strict requirements of 24-hour uninterrupted production and storage in the cold chain.

The unit is equipped with an industrial-grade PLC intelligent control system, supporting multi-level energy regulation, with the cooling capacity able to be smoothly adapted within a wide range, precisely matching the differentiated temperature zone requirements of preservation, refrigeration, and low-temperature rapid freezing; it supports local touch operation, remote data monitoring, automatic fault alarm, and operation data traceability, and can be connected to the factory's intelligent management platform, enabling unmanned operation and preventive maintenance, reducing on-site operation labor costs. At the same time, it is compatible with mainstream environmentally friendly refrigerants such as R507A and R404A, suitable for food and pharmaceutical industry clean control standards, and can be used in conjunction with rapid freezing tunnels, flat rapid freezing machines, and multi-temperature zone cold storage warehouses.

The product is suitable for a wide range of scenarios, covering pre-prepared food processing industrial parks, aquatic product low-temperature processing, meat slaughtering rapid freezing, large-scale cold storage logistics warehouses, pharmaceutical GSP constant-temperature warehouses, chemical process cooling, etc., suitable for new cold chain projects as well as energy-saving renovations of old cold storage refrigeration systems, with modular design supporting on-demand expansion, and adaptable to the step-by-step expansion of enterprise production capacity.

Under the background of the green and low-carbon transformation of the cold chain industry and the increasingly strict safety management of food processing, the screw parallel compression condensing unit, with its core advantages of intelligent group control energy saving, redundant reliability, and convenient operation and maintenance, solves the problems of high energy consumption, high shutdown risk, and difficult expansion in large and medium-sized refrigeration projects, continuously empowering the high-quality development of industries such as pre-prepared food, aquatic product cold chain, and pharmaceutical storage, and creating a stable, efficient, and safe underlying refrigeration equipment support for the cold chain system.

Read More
2026-07-08
Hydraulic Contact Fresh-Locking, Energy-Efficient Quick Freezing | New-Generation Hydraulic Plate Freezer Empowers Processing Upgrade for Aquatic Products and Prepared Dishes.

Recently, focusing on the upgrading of food cold chain equipment, the new-generation hydraulic plate freezer has been officially launched to the market. Adopting the hydraulic compression contact quick-freezing principle, the equipment features uniform freezing, low dehydration loss, controllable energy consumption and compact structure. It is suitable for the industrial quick-freezing of block-shaped raw materials including aquatic products, poultry meat and prepared food, delivering low-loss, high-quality fresh-locking solutions for food processors and helping the quick-freezing industry improve quality, efficiency and revenue while cutting costs.

In food quick-freezing processing, conventional blast freezing commonly suffers from high dehydration loss, uneven freezing and juice loss of raw materials, which directly affect the finished product yield and market selling price. This hydraulic plate freezer adopts a hydraulically driven compression structure. With adjustable pressure, it enables tight contact between food and high-thermal-conductivity aluminum alloy freezing plates to eliminate air insulation gaps. It achieves rapid temperature reduction via double-sided direct contact heat transfer, forming fine ice crystals quickly to fully preserve the cellular structure of raw materials. It maximally retains the original flavor, juice and nutrition of ingredients, greatly reduces product dehydration loss, and improves the yield rate and premium value of finished products.

The core freezing plates of the equipment are made of food-grade aluminum alloy with outstanding thermal conductivity and high heat exchange efficiency. The frame, pipelines and chamber body of the whole machine adopt SUS304 stainless steel, paired with high-density polyurethane insulation layers for excellent cold retention performance. It meets hygienic standards for food contact, with smooth surfaces easy to rinse and sanitize, suiting the routine cleanliness management requirements of food factories. Equipped with an independent hydraulic station and hard-chrome wear-resistant cylinders, it delivers stable lifting and compression with adjustable pressure and low leakage risk. Built-in intelligent electronic control system supports customized freezing duration and temperature parameters, realizing the full process of compression, quick freezing, pressure relief and discharging with one click. It is easy to operate and can be monitored by a single operator, applicable to multiple scenarios such as onshore processing plants and ocean-going fishing vessels.

Compared with tunnel quick-freezing equipment, the hydraulic plate freezer features a compact structure and smaller footprint. It requires no high-flow supporting fans and achieves lower overall energy consumption, making it flexible for renovation projects with limited space in small and medium processing plants, aquatic terminals and fishing vessel decks. It is widely used for quick-freezing of aquatic products such as fish fillets, fish paste, shrimp and shellfish, as well as cut meat, small-packaged poultry, boxed prepared dishes and fruit & vegetable blocks. It serves as the preferred fresh-locking equipment for standardized processing of export aquatic products and prepared food, delivering neatly shaped and stable-quality frozen products that satisfy the high standards of foreign trade orders.

Read More
Certificate Of Honor
  • High-tech Enterprise Certificate